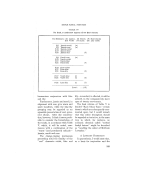
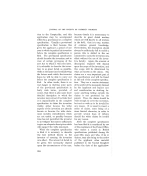
JOURNAL OF THE SOCIETY OF COSMETIC CHEMISTS It is useful to calculate the average number of positives in the population which will give various expectations of obtaining 0 positives in the sample group of test subjects. These results are tabulated as follows ß Number cf reactions found... nil Average number of With a sample of size 200, an positives to be expected Expectation of obtain- average of one positive would in the sample ing 0 reactions be found in every n of the population , . 4.61 0.01 43 3.00 0.05 67 2.30 0.10 87 1.00 0.37 200 0.70 0.50 285 0.11 0.90 1,818 0.05 0.95 4,000 0.01 0-99 20,000 0 reactions over this probability range could mean any average number of positives ranging from 1 in 43 to 1 in 20,000. Thus, in 10 tests out of every 100 tests 0 reactions would be found in a sample of size 200, when actually the average of the whole population could be as much as 1 in 87. This means that, once in ten tests giving 0 reactions from 200 test subjects, the product will be passed, although it will produce throughout the whole population represented by the sample an average of one reaction in every 87. This would be an appalling mistake even for the cosmetic industry, and it shows the necessity for a more extensive test or for an alternative one. DODGE AND ROMIG SAMPLING TECHNIQUE Dodge and Romig' have developed from the Poisson distribution two sampling schemes ß single and double sampling. The object of these schemes is to maintain the quality of a large population of objects at an agreed "process' average percentage defective" by inspecting a sample taken from the whole population. The risk which the consumer is willing to take-- i.e., that the percentage of the defective objects in any batch (usually called the "lot") of the population which the sample purports to represent does not exceed his limit "lot tolerance per cent defective"--is called the "consumer's risk." By Dodge and Romig's single sampling method the sample is inspected, and if the rejects exceed a certain number the lot is either rejected at once or else the whole of the remainder of the lot is examined. In their double sampling scheme a smaller sample is inspected, and if the rejects exceed a certain number a second sample is taken and the number of rejects found in it added to those in the first sample. Should the combined rejects exceed 226

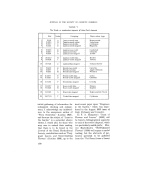
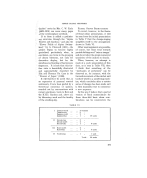
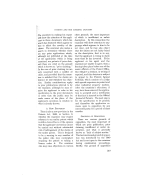
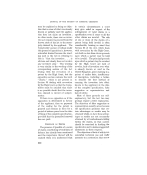
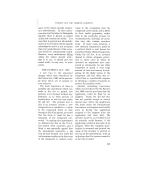
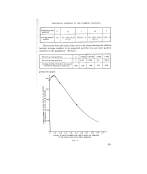
STATISTICAL METHODS IN THE COSMETIC INDUSTRY ?[ certain value, the whole lot is either rejected or given 100 per cent : ?iinspection. These schemes can be adapted to the prophetic patch test. Let us assume that we do not wish to market a product wkich will give more than 0.05 per cent contact dermatitis reactions. This is really much too high, as no'product would survive 1 in 2,000 complaints about dermatitis. We wish to be sure that not more than once in ten times will a product pass our test, if it !i•i•?::will give more than 0.5 per cent cases of contact dermatitis. Thus our process average per cent defective is 0.05 per cent, our lot tolerance per cent defective 0.5 per cent, and our consumer's risk 0.10. In this case our lot size is a con- venient number of the product, such as those expected to be sold in a given period, e.g., if sales are expected to be 10,000 a week with, in our case of ??.0.05 per cent process average per cent defective, an average number of ilerrnatitis cases of 50(!) per week, the lot size is 10,000. Reference to Dodge and Romig's Table 1 gives the following relevant data' Lot tolerance per cent defective--0-5 per cent. Process average per cent defective--0.05 per cent. Number of positive Maximum average per Lot Size Size of Sample to reactions not to be cent reactions given by be inspected exceeded whole of population .... _ 301-400 275 0 0.04 401-500 300 0 0.05 501-600 320 0 0-05 601-800 350 0 0-06 801-1,000 365 0 0.06 1,001-2,000 410 0 0.07 2,001-3,000 430 0 0.07 3,001-4,000 440 0 0-07 4,001-5,000 740 1 O. 10 5,001-7,000 750 1 0.10 7,001-10,000 760 1 0.10 10,001-20,000 775 1. O- 10 20,001-50,000 1,050 2 O. 13 50,001-100,000 1,060 2 O. 13 Thus, in our example, for a lot size of 10,000, we should carry out patch tests on 760 people and get not more than one positive reaction, giving us a one in ten risk that the 10,000 would not contain more than 50 (i.e., 0.5 per cent) individuals with positive reactions, and that the average number of reactions from many lots of 10,000 would be 5 li.e., 0.05 per cent). This is a large number of tests to carry out for such small results, but they can be reduced by using the double sampling technique. Using the same values as in the above example, Dodge and Romig's Table II gives the following data: 227
Purchased for the exclusive use of nofirst nolast (unknown)
From: SCC Media Library & Resource Center (library.scconline.org)